Endless vs Open-Ended vs Spliced Timing Belts: Construction Types and Applications
Endless vs Open-Ended vs Spliced Timing Belts: Which Construction Fits Your Machine?
How each timing belt construction is made, where it wins, and how to join open-ended belts without losing pitch accuracy
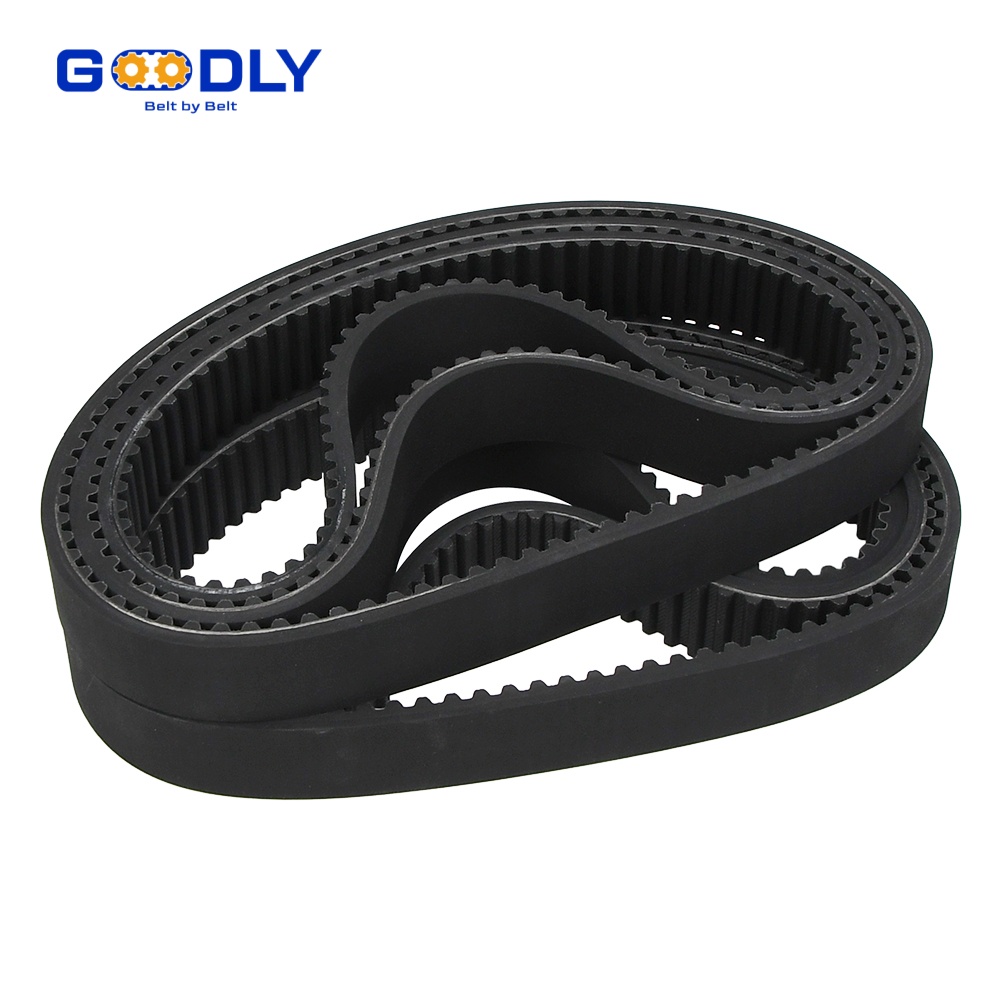
Every timing belt starts life as one of three constructions: a truly endless timing belt moulded as a continuous loop, an open-ended timing belt supplied as a straight length, or an open length that is spliced or welded into a loop on site. The choice decides your maximum centre distance, your pitch accuracy, your tension stability and your spare-part strategy. Pick wrong and a 12-metre conveyor ends up with a joint that walks off the pulley every shift; pick right and the belt disappears into the machine and is forgotten for years. This guide compares all three constructions, explains timing belt joining methods, and shows step by step how to connect an open ended timing belt for conveyor applications.
Open-Ended Timing Belt vs Endless Timing Belt: What Fits Your Machine?
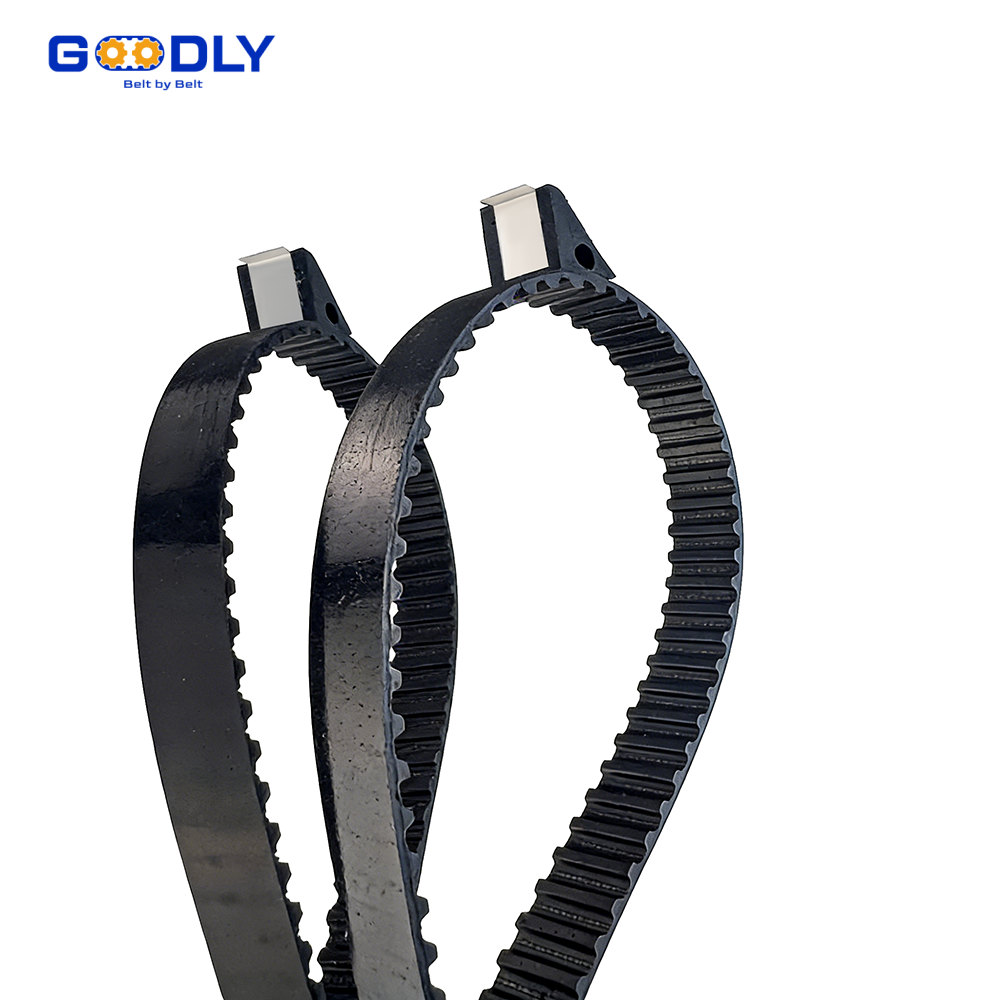
The decision is mostly geometry. A closed-loop, truly endless timing belt must slide over the pulleys or the machine must be designed around it, so it suits fixed-centre-distance drives where the frame can be opened or the belt installed at build time. An open-ended timing belt ships as a straight cut length, threads through idlers and along the frame of a long linear or conveyor system, and is then joined — or left open and clamped at both ends, as in many linear actuators where the carriage is the “pulley”.
| Criterion | Truly endless | Open-ended (clamped) | Open-ended, spliced/welded |
|---|---|---|---|
| Max centre distance | Limited by mould, typically to ~2-3 m | Unlimited (frame length) | Unlimited |
| Pitch accuracy | Highest — no joint | High, set by clamp position | Good; joint must be squared |
| Tension member | Continuous cords | Cut cords at clamps | Welded butt joint |
| Install / replace | Machine open-up needed | Fastest, no disassembly | Welding kit or factory splice |
| Typical cost | Lowest per loop | Low; hardware adds cost | Higher (joining labour) |
| Best fit | Power transmission drives | Linear positioning | Long conveyors, accumulation |
A quick rule: if the belt transmits power between two shafts at a fixed distance, specify endless; if the belt carries product over a distance or positions a carriage, open-ended wins. Material plays in too — compare rubber and PU grades in our timing belt materials guide.
Truly Endless Timing Belt Advantages: Strength, Life and No Joint Weakness
A truly endless timing belt is vulcanised or moulded in one pass, so every glass, aramid or steel cord runs continuously around the loop with no cut ends. That single difference drives three advantages:
- Full cord strength. With no splice, the tension member carries 100% of its rated load around the whole loop — no derating, no weak point.
- Uniform belt life. Every tooth position sees identical cord support, so wear spreads evenly instead of concentrating at a joint.
- Stable tension. A continuous cord set means modulus is identical everywhere, so pre-tension set at install stays consistent through the belt’s life.
The trade-offs are installation and inventory: an endless rubber timing belt must pass over the pulley end or the frame must split, and each special length is a moulded part rather than a cut from stock. For high-torque drives where a joint would be the first thing to fail, that trade is worth it every time. See also our guide on vulcanised timing belts for how the endless loop is consolidated under heat and pressure.
Spliced and Welded Timing Belt Joining Methods for Open-Ended Belts
When an open length must become a loop, three timing belt joining methods dominate. For pu spliced timing belt construction, the thermoplastic polyurethane body is butt-welded with a heating plate or hot knife while the cords are butted — never overlapped — so pitch is preserved; joint efficiency typically reaches 85-95% of base belt strength. Mechanical fasteners suit thick rubber conveyor belting but are rarely used on toothed synchronous belts because the clip disturbs tooth mesh. Finally, factory vulcanised splices are made on GOODLY’s press before shipping, giving a loop without an on-site welder.
Heat-plate welding
Standard for PU open-ended belts; clean, flexible joint with ~90% strength.
Mechanical fasteners
Fast field repair for rubber conveyor belts; not for precision tooth mesh.
Factory vulcanised splice
Cured on press before dispatch; near-seamless loop, no site work.
How to Connect Open-Ended Timing Belts for Conveyor Applications
Here is the field procedure our customers use for a welded PU conveyor loop. Follow it and the joint will run true from the first shift:
- Cut to length with cord awareness. Calculate pitch length exactly, then cut square to the belt edge with a sharp knife or hot cutter — a ragged cut becomes a tracking fault.
- Square the ends. Clamp both ends in a joining jig and check the diagonal; a 1 mm error across a 100 mm belt shows up as lateral drift within metres of running.
- Butt the cords, never overlap. Overlapping cords thickens the joint, changes its pitch and hammers the pulley grooves once per revolution.
- Weld with correct temperature and dwell. Use the belt maker’s plate temperature and dwell time; overheat embrittles the PU, underheat gives a cold weld that peels at the tooth root.
- Dress the joint. Remove the weld bead flush to the belt surface so the backside runs cleanly over knife edges and idlers.
- Tension, track, then re-check. Apply recommended pre-tension, run the belt slowly over the full loop and re-check the joint after the first hour.
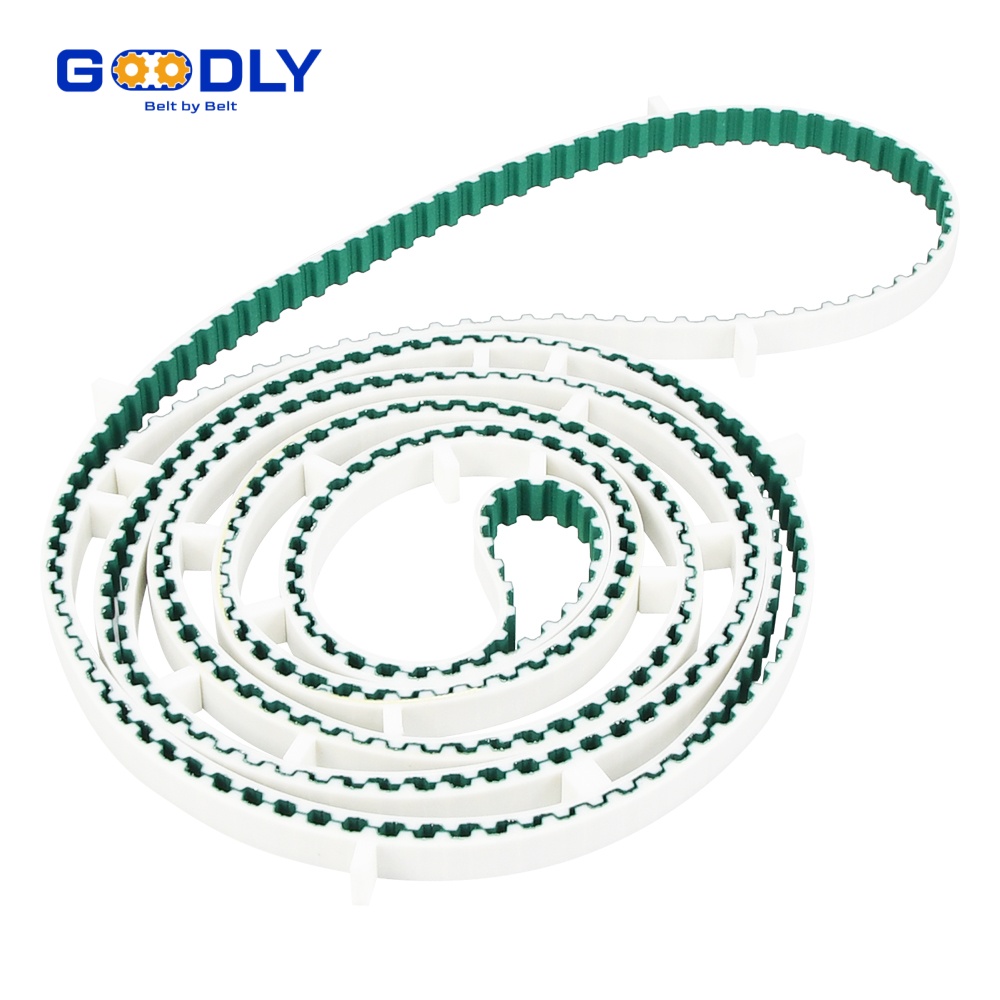
If site welding is not practical, order the loop factory-spliced from our special machining line, where slitting, welding and finishing happen under controlled conditions.
Which Timing Belt Construction Do Machine Builders Specify Most?
Across the packaging, printing and automation machines we quote each week, the split is remarkably stable. Endless loops dominate power-transmission positions; open-ended PU dominates linear and long-bed conveying. What changes by industry is the finish — coatings, profiles and machining, all documented in our timing belt overview.
| Industry / machine | Dominant construction | Why |
|---|---|---|
| Packaging machinery | Endless + coated endless | Fixed shafts, hygienic loop, quick swap |
| Printing & paper converting | Truly endless, machined | Zero-joint accuracy at speed |
| Linear motion / robotics | Open-ended PU, clamped | Carriage tensioning, cut to frame |
| Long product conveyors | Open-ended PU, welded loop | Centre distance beyond moulded sizes |
| Food & pharma transport | Endless with silicone/sponge backing | Heat, release and washdown |
Machine builders standardise on construction families early, then vary width, coating and machining per project — which is why our timing belts with special machining page pairs with every construction type above.
Ask GOODLY: Endless, Open-Ended or Spliced for Your Drive
Send us the centre distance, pitch, width, load and environment, and our engineers will reply with the construction we would run in our own machines — endless, clamped open-ended or a welded pu spliced timing belt — plus a drawing within 48 hours. Samples cut from stock lengths ship in 3-5 days so you can validate tracking before committing to tooling.
Can any open-ended timing belt be welded into a loop?
Thermoplastic PU belts weld cleanly. Rubber open-ended belts are usually supplied with factory-vulcanised splices or mechanical clamps, because rubber does not heat-weld reliably on site.
How much strength does a welded joint keep?
A properly made PU heat-weld butt joint typically retains 85-95% of base belt tensile strength; a factory splice can exceed that because cords and coating are consolidated under press conditions.
Do open-ended belts lose timing accuracy?
No. The teeth and pitch are identical along the length; accuracy depends on how squarely the ends are cut and joined, which is why we jig-check every splice.
What is the longest open ended timing belt you supply?
We cut PU and rubber open lengths to order — well beyond 100 metres — and can weld loops to your exact pitch length on request.
Not Sure Which Construction Your Drive Needs?
Send your drawing or centre distance to GOODLY’s engineers. We compare endless, open-ended and spliced options for your application, quote within 48 hours and ship samples in 3-5 days.
Request a Free Construction Review