We manufacture and customize industrial
motion belts to precisely match mainstream
equipment worldwide.
 Rubber Timing Belt
 PU Timing Belt
 Silicone Timing Belt
 Silicone Vulcanized Timing Belt
 Vulcanized Timing Belt
 Sponge Timing Belt
 Timing Belts with Special Machining
 Rubber Flat Belt
 PU Flat Belt
 Nylon Flat Belt
 Foam Flat Belt
 Vulcanized Flat Belt
 PU Conveyor Belt
 PVC Conveyor Belt
 Rubber Conveyor Belt
 Sponge Conveyor Belt
 Conveyor Belts with Special Machining
 Timing Belt Pulley
 Rod-Shaped Synchronous Timing Pulley
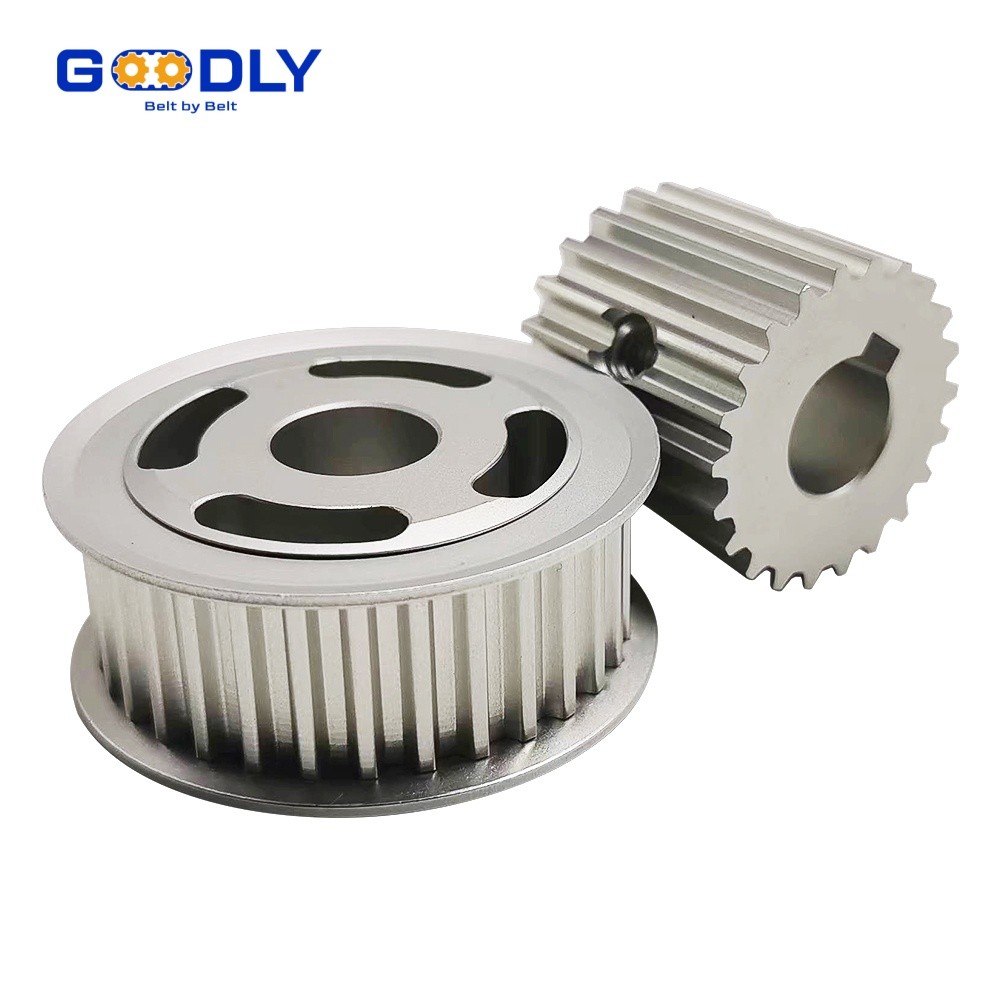 Surface-Pressure-Bearing Timing Pulley
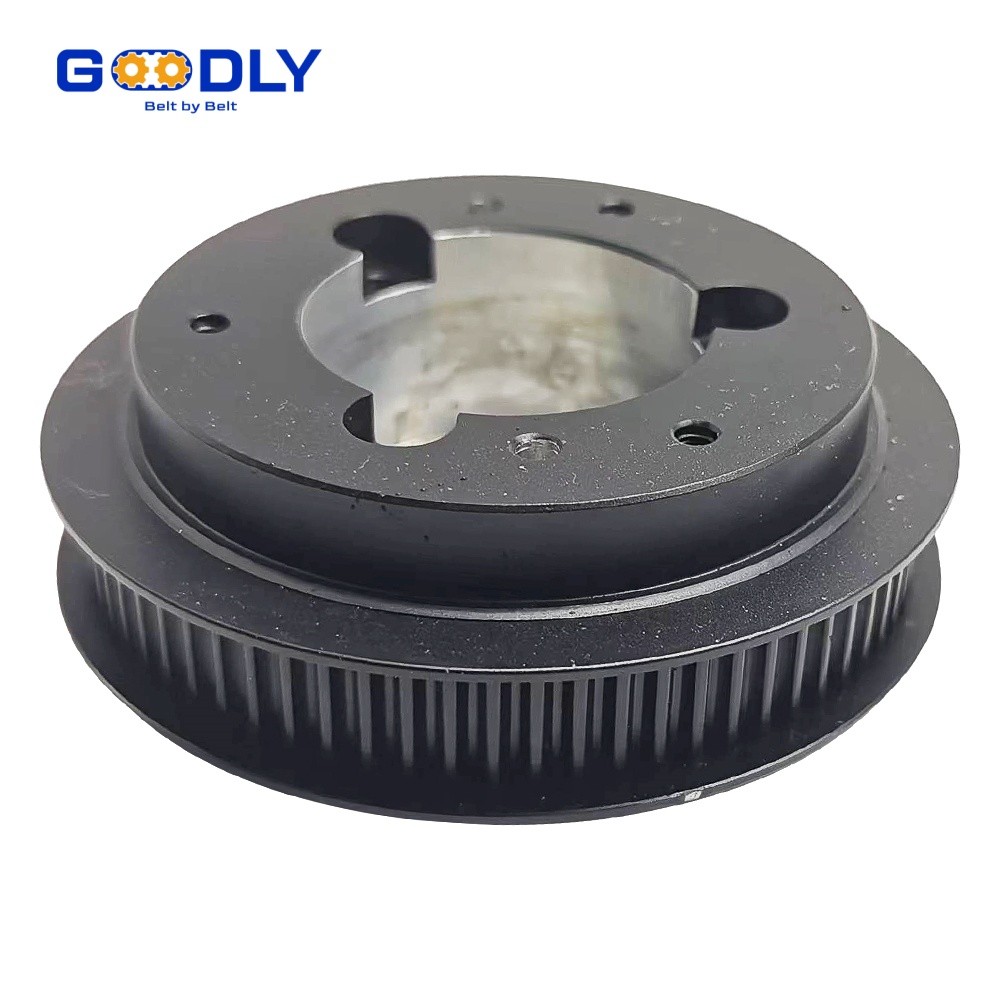 Serrated Idler Gear Timing Pulley
 Multi-Groove Belt
 V-Belt
 PU Round Belt
How should belt ends be prepared before vulcanizing a joint?
Direct answer: A good joint is decided before the press is closed: both ends must be cut square to the belt axis, the joining surfaces buffed evenly and kept clean and dry, and the correct adhesive or uncured rubber applied in the right order. Skewed cuts, oily surfaces and rushed cure cycles cause more early failures than the press itself.
The six preparation steps that decide joint quality
- Measure and mark: lay the belt flat and mark the cut line exactly square to the belt edge. A mis-cut of two or three degrees already shows up as running-off-centre later.
- Cut square: use a sharp knife with a guide or a cutting jig. On thicker belts, cut in several shallow passes instead of forcing one heavy cut.
- Buff to a uniform finish: roughen the joining surfaces evenly, removing only the depth of material the procedure calls for. Shiny glazed spots or deep gouges both weaken the bond.
- Clean and dry: brush off the buffing dust and wipe with an approved cleaner, then let the solvent flash off completely. Any residue stays between the layers forever.
- Apply the adhesive system: follow the belt specification for primer, cement and uncured cover rubber, and respect the drying time between coats.
- Press with the correct heat and time: close the vulcanizing press at the specified temperature and pressure and hold the full cure time. Opening early to peek saves minutes and can cost the whole joint.
Checklist before you close the press
| Check | What good looks like |
|---|---|
| Cut angle | Square to the belt edge within about one degree, on both ends |
| Buffed surface | Even roughness, no shiny spots, no deep gouges |
| Cleanliness | No dust, oil or fingerprints; solvent fully flashed off |
| Adhesive | Correct primer and cement for the belt type, full drying time respected |
| Cure cycle | Temperature and pressure held for the full specified time |
If on-site vulcanizing is not practical in your plant, the belt can be supplied already vulcanized to your required length at the factory, so the joint is made and inspected before it ships.
Send your belt details
Email sales@goodlybelts.com with the belt type, width, thickness and operating conditions, or use the enquiry form. We will confirm the right joint type for your belt and, if you prefer, quote it factory-vulcanized to length.
Ask about vulcanized joints
Are you looking for a reliable manufacturer of conveyor belt products?
We can quickly provide customers with market analysis, technical support and customized services.We manufacture and customize industrial
motion belts to precisely match mainstream
equipment worldwide.
Please send your message to us
- Name
- Phone
- *Title
- *Content